English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek
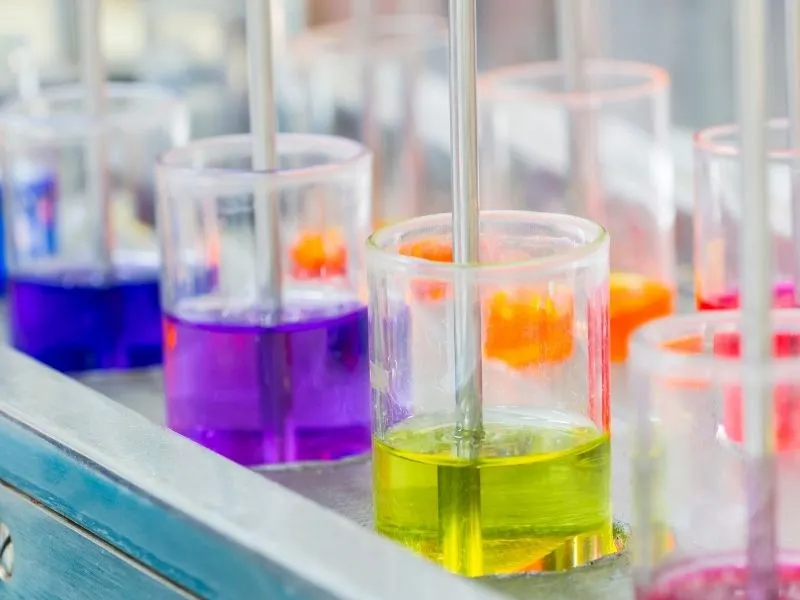
A reliable solvent dyes supplier plays an important role in industries that require high-quality colorants for plastics, coatings, inks, fuels, lubricants, and other solvent-based applications. Solvent dyes are specialized colorants that dissolve in suitable organic solvents rather than remaining as insoluble particles. Their ability to produce transparent colors, strong color intensity, and uniform coloration makes them valuable for manufacturers seeking consistent results across a wide range of products.
Choosing the right solvent dye manufacturer or distributor can help businesses maintain product quality, improve processing efficiency, and meet specific application requirements. Different industries need different dye characteristics, including solubility, color strength, thermal stability, light resistance, and compatibility with particular materials. A knowledgeable supplier can help customers identify suitable colorants based on their formulations, production methods, and final product specifications.
As industrial markets continue to develop, manufacturers are increasingly focused on product consistency, reliable sourcing, and cost-effective production. A professional solvent dyes supplier can support these objectives by offering dependable products, technical documentation, and guidance on selecting appropriate dye grades. Establishing a strong supplier relationship can also help businesses manage inventory, maintain production schedules, and respond to changing customer demands.
Industrial Applications and Benefits of Solvent Dyes
Solvent dyes are widely used in applications where transparent coloration, good compatibility, and consistent color appearance are important. Unlike many conventional pigments, which remain dispersed as solid particles, solvent dyes dissolve in compatible liquid media. This characteristic makes them particularly useful in systems where clarity and uniform color distribution are essential.
The plastics industry is a major application area for solvent colorants. Manufacturers use suitable solvent dyes to color certain engineering plastics, acrylic materials, and other compatible polymer systems. These colorants can help produce transparent or translucent components with attractive visual properties. The correct dye selection depends on the polymer type, processing temperature, chemical composition, and required end-use performance.
In the coatings and printing industries, solvent dyes may be used in selected formulations that require transparent color effects. They can contribute to consistent coloration in specialized coatings, decorative finishes, and certain printing inks. Manufacturers must evaluate dye compatibility with the resin, solvent system, and other formulation ingredients to avoid unwanted changes in appearance or performance.
Solvent dyes also have applications in fuels, oils, lubricants, and industrial liquids. Suitable colorants can help distinguish products, support product identification, and provide a recognizable appearance. In these applications, the dye must be compatible with the liquid medium and maintain appropriate color stability during storage and use. Product specifications should be checked carefully because not every solvent dye is suitable for every fuel, oil, or lubricant.
A dependable solvent dyes supplier can help manufacturers identify colorants that meet their application requirements. Important performance characteristics include solubility, color strength, shade consistency, thermal stability, and resistance to light or chemicals where relevant. The importance of each property depends on the product being manufactured and the conditions it will experience during processing and use.
Selecting the Right Solvent Dyes Supplier for Industrial Needs
Choosing a suitable solvent dyes supplier requires attention to product quality, technical expertise, supply reliability, and compatibility with the intended application. Businesses should evaluate whether the supplier offers dye grades appropriate for their industry and whether the products meet their required technical specifications.
Consistent quality is especially important for manufacturers producing goods in repeated batches. Differences in dye concentration, shade, or solubility can affect the final product and create unnecessary adjustments during manufacturing. Suppliers with effective quality control procedures can help businesses maintain predictable results and reduce the risk of production interruptions.
Technical support is another important factor. Solvent dyes must be selected according to the chemistry of the application. A dye suitable for a particular plastic may not perform effectively in a fuel, coating, or printing ink. A knowledgeable supplier can provide technical data, recommend appropriate grades, and help customers assess compatibility with their formulations. Sample testing is often useful before a product is introduced into full-scale production.
Businesses should also examine product documentation. Technical data sheets provide information about relevant product characteristics and recommended applications, while safety data sheets describe hazards, handling precautions, storage conditions, and emergency measures. Clear documentation supports safer chemical management and helps manufacturers evaluate whether a product meets their operational requirements.
Supply chain performance should not be overlooked. Delayed deliveries can affect production schedules, especially when a specific dye grade is essential to a manufacturing process. A dependable supplier should communicate clearly about availability, packaging, order quantities, and delivery timelines. Consistent communication can help manufacturers plan purchasing activities and reduce the risk of material shortages.
Cost-effectiveness is another consideration when comparing solvent dye suppliers. The lowest purchase price does not necessarily provide the best overall value. Manufacturers should consider color strength, dosage requirements, compatibility, processing performance, and the potential costs associated with inconsistent quality. A suitable dye may improve production efficiency and reduce avoidable waste when used under appropriate conditions.
Solvent Dye Quality, Storage, and Future Industry Trends
Proper storage and handling are essential for maintaining the quality of solvent dyes. Manufacturers should follow the supplier's recommendations regarding temperature, moisture exposure, packaging, ventilation, and storage conditions. Containers should remain appropriately closed when not in use, and materials should be protected from contamination. Specific precautions depend on the chemical properties of the product and the requirements described in its safety documentation.
Before using a new solvent dye, manufacturers should evaluate its performance under their actual production conditions. Laboratory testing can help assess solubility, shade accuracy, compatibility, and stability. For applications involving elevated processing temperatures or exposure to light and chemicals, additional testing may be necessary to confirm that the selected dye meets the required performance standards.
Environmental responsibility is also receiving greater attention in the colorant industry. Manufacturers are evaluating chemical handling practices, solvent management, waste reduction, and compliance with relevant environmental regulations. A responsible solvent dyes supplier can support these efforts by providing accurate product information and documentation that helps customers make informed purchasing decisions.
Developments in polymer technology, coatings, printing, and specialty chemical formulations continue to create demand for application-specific colorants. Manufacturers increasingly require precise shades, reliable batch consistency, and dyes that perform effectively within specialized formulations. Improved laboratory testing and digital color measurement can help businesses achieve more accurate color matching and reduce the need for repeated formulation adjustments.
Long-term cooperation between manufacturers and suppliers can make it easier to address these changing requirements. By communicating application needs, conducting product trials, and reviewing performance results, businesses can identify suitable dye grades and improve their production processes. Reliable sourcing and effective technical collaboration can support consistent quality while helping companies adapt to evolving industrial expectations.
Conclusion
Selecting a professional solvent dyes supplier is an important step for businesses that depend on consistent coloration, reliable chemical performance, and efficient industrial production. Solvent dyes serve a variety of applications, including plastics, coatings, printing inks, fuels, oils, and other compatible solvent-based systems. Their suitability depends on the chemical formulation, processing conditions, and performance requirements of the finished product.
A dependable supplier should provide consistent product quality, appropriate technical documentation, application guidance, and reliable deliveries. Manufacturers should carefully evaluate solubility, color strength, compatibility, stability, storage requirements, and overall cost-effectiveness before selecting a dye.